
While flavour and formulation often capture the spotlight, the systems that keep confectionery moving—from conveyors to end-of-line packaging—are increasingly central to a brand’s ability to compete. The mechanics of motion, once seen as background infrastructure, have become strategic assets in meeting modern market demands.
Flexibility now rivals throughput as a top priority. Manufacturers must respond to fast-changing trends, accommodate a growing array of product formats, and meet strict hygiene standards—often within the same production shift. At the same time, environmental considerations are influencing every aspect of packaging, from material choice to the machines that handle it. The convergence of these pressures is reshaping expectations of what conveyor and packaging systems must deliver.
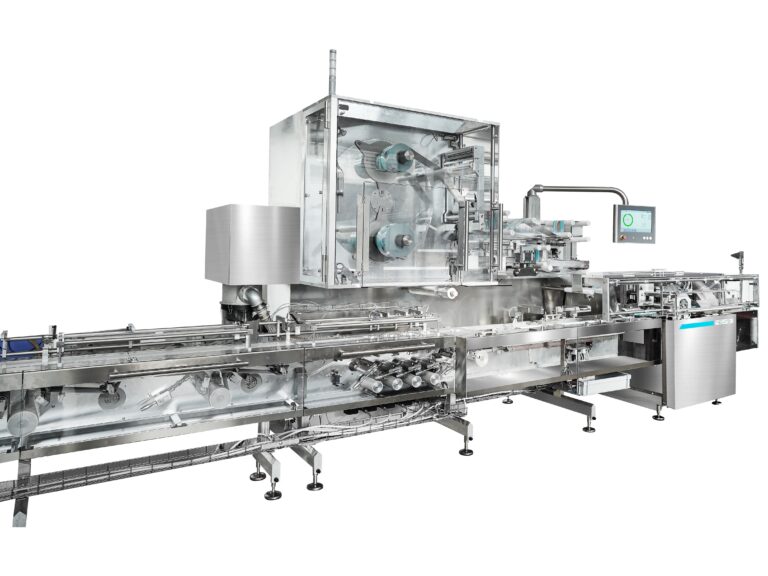
Technology providers are answering the call with solutions that blend hygiene, efficiency, and smart automation. Modular conveyor systems from companies like Ammeraal Beltech and Intralox are helping producers reduce downtime and enhance cleanability. Innovations from Ishida, Mpac Langen, and IPCO AB are enabling more compact, integrated, and data-rich lines, while Berndorf is advancing belt technologies that bring intelligence to the production floor.
Thanks to forward-thinking manufacturers like these, a new generation of conveying and packaging solutions is helping confectionery manufacturers achieve not only higher efficiency, but also the agility and sustainability required to stay competitive in an industry that refuses to stand still.
Built for Hygiene, Speed, and Adaptability
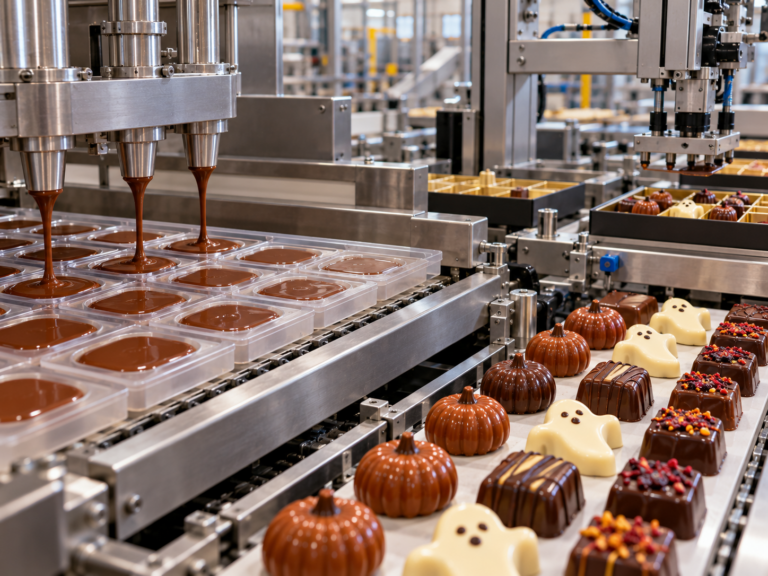
The conveyor may be one of the most overlooked assets on the factory floor, yet in today’s confectionery production environment, it plays a pivotal role in ensuring operational resilience, hygiene compliance, and production agility. With the demands on manufacturers to offer greater product diversity and faster changeovers, modern conveyor systems are no longer static transport mechanisms—they are dynamic, intelligent platforms designed to accommodate everything from soft-centred chocolates to sugar-dusted jellies with precision and care.
One of the most significant shifts has been the move toward modular and reconfigurable conveyor systems, allowing producers to switch between formats with minimal downtime. As seasonal products, limited editions, and consumer-driven variations become the norm, this modularity enables smaller batch runs and frequent changeovers without compromising efficiency. Companies like Ammeraal Beltech have responded with hygienic belt systems that offer tool-free maintenance, enhanced cleanability, and rapid belt replacement—key features for confectioners working with sticky, sugary, or allergen-sensitive products.
Intralox, a global leader in conveying technology, has developed its Activated Roller Belt™ (ARB) systems to handle multi-directional sorting, accumulation, and merging—without the need for complex mechanical diverting. These intelligent systems reduce mechanical wear while improving line speed and reducing footprint, making them ideal for high-throughput confectionery plants where space is at a premium.
Cleanability has become a non-negotiable standard, especially given the heightened awareness of food safety and allergen management. In environments where sugar residues, syrups, and fat-based coatings are commonplace, cleaning efficiency can make or break production uptime. IPCO AB provides steel belt systems designed not only for robust thermal performance but also for their clean-in-place capabilities, which help ensure that cooling and transport phases meet strict hygiene standards without compromising mechanical stability.
Advanced conveyors are now increasingly integrated with upstream and downstream systems—such as formers, coaters, and packaging lines—creating a more seamless and synchronised flow. This integration is critical for managing delicate confectionery products that are sensitive to pressure, temperature, or mishandling. At the same time, digital sensors and real-time data capture are giving operators greater visibility into belt performance, temperature fluctuations, and load distribution, which supports predictive maintenance and continuous improvement strategies.
Automation in Motion
Automation is moving beyond the packaging zone and embedding itself throughout the line—including the conveyors themselves. Today’s production environments demand not just speed, but intelligence. Real-time feedback, digital coordination, and predictive control are transforming how confectionery moves from one phase of processing to the next.
Conveyor systems are increasingly fitted with smart technologies—sensors, AI-enabled controllers, and advanced actuators—that allow them to do more than simply transport products. These intelligent systems can now sort, redirect, accumulate, or reject items autonomously based on visual inspection or line conditions. This functionality becomes particularly valuable in facilities managing multiple SKUs with varying shapes, textures, and packaging requirements.
For instance, Intralox’s integration of smart sensors and edge computing capabilities enables their conveyors to collect performance data continuously. This not only supports real-time decision-making—such as adjusting speeds based on line flow—but also enables predictive maintenance, reducing the risk of unexpected downtime. Their solutions are especially relevant for high-speed environments where product flow must remain uninterrupted, even as line configurations shift throughout the day.
Another key innovation lies in belt monitoring systems. Berndorf, known for its advanced steel belt technologies, is incorporating smart detection tools into their conveyor platforms. These include systems that track belt wear, surface damage, and temperature stability—all critical for confectioners working with thermally sensitive products such as caramel, nougat, and chocolate layers. By detecting early signs of mechanical stress or contamination risk, such systems help extend belt life and reduce the need for reactive repairs.
Moreover, automation is enabling seamless integration between conveying and inspection systems. Conveyor-mounted cameras and sensors—often tied to AI-powered inspection units—can detect product anomalies such as misalignment, missing items, or packaging defects. Once detected, conveyors automatically reroute or isolate those items for further inspection or rejection, maintaining product integrity without slowing down the line.
Digital connectivity is another area of growth. Conveyor systems are now routinely integrated into plant-wide SCADA (Supervisory Control and Data Acquisition) and MES (Manufacturing Execution Systems) networks. This allows operators and managers to monitor performance KPIs like throughput, reject rates, and energy usage from a central dashboard, facilitating faster decision-making and cross-line optimisation.
Read the full article in our latest issue here