IPCO’s steel belt conveyor systems combine hygiene, reliability and flexible design to support efficient chocolate production in demanding industrial environments
In some industries, conveying is a purely functional process involving the transportation of goods from one point to another. In chocolate production, it is much more than this.
Every transfer point can affect product integrity, hygiene, line efficiency and production uptime. When chocolate products need to be moved between cooling, forming, buffering, distribution, further processing or packaging, manufacturers need a conveying system that is reliable, accessible and engineered around their actual process.
Tailor-made handling
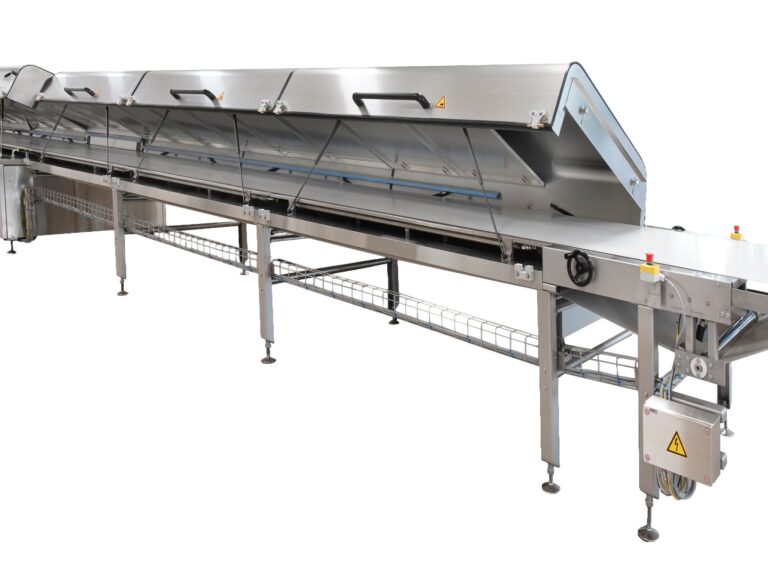
IPCO steel belt conveyors provide robust, hygiene-focused, and tailor-made handling for a wide range of chocolate products including drops, chunks, chips, inclusions, compound products, nut-based or filled items, and semi-finished chocolate products requiring controlled transfer to downstream equipment.
IPCO is unique in being the only company in the world able to manufacture and supply both the steel belt and the conveyor. With over 1,100 chocolate conveyors installed across 60 countries, the company’s solutions offer the reassurance of performance proven in real industrial chocolate production environments.
Systems can be configured to handle throughputs ranging from approximately 2,700 kg/h up to 10,000 kg/h, with operating speeds up to 70 m/min for the most demanding production environments. Typical belt widths are 400 mm and 500 mm. A comprehensive range of belt tracking technologies, controlled drive systems, belt support components and cleaning systems ensures dependable long-term operation.
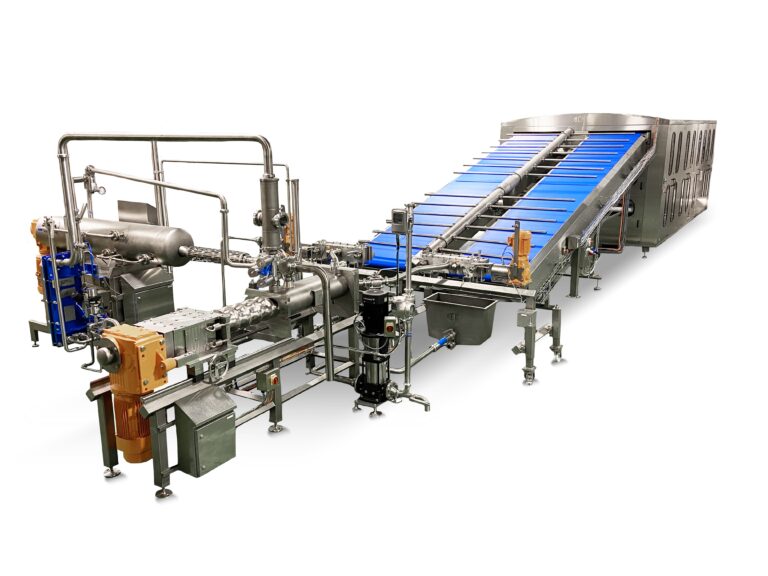
A high degree of design flexibility enables conveyors to be engineered around a customer’s specific requirements, taking to account factors such as factory layout, available space, product flow, inlet/outlet heights, required incline, discharge configuration and downstream process. This also allows for seamless integration into both new production lines and existing installations.
Inclined conveyor sections can support product elevation between process levels, while pneumatic diverters can be used to distribute product to multiple discharge points. This flexibility is invaluable in factories where product must be transferred to different conches, bins, buffers, packaging lines or other downstream equipment.
Hygiene is a critical priority in food production and steel belt conveyors can be engineered to meet the most stringent of standards. Design options include stainless steel side protections, transparent cover hoods for visibility and protection, and belt cleaning systems. Features such as PE-HMW belt support and product contact components, and AISI 304 stainless steel discharge hoppers further underscore the focus on a hygiene-conscious design, ensuring that the conveyor is practical and accessible for daily maintenance.
“Chocolate production depends on stable and continuous product flow,” explains Mitchell Paquaij, Global Segment Manager, Chocolate at IPCO. “IPCO steel belt conveyors are tailor-made to move product reliably between process steps, helping manufacturers reduce interruptions, support line efficiency and maintain continuous operation.”
“These systems are not standard transport conveyors. They are engineered around the customer’s product, process flow, production capacity, factory layout and downstream requirements.”
IPCO’s steel belt conveyors are built around a robust and stable steel belt surface designed for continuous industrial operation. This makes them especially relevant for chocolate manufacturers looking for reliable product transfer at higher capacities, longer conveying distances, elevated discharge points or complex line layouts.
IPCO also supports customers with lifecycle services including inspections, maintenance, spare parts supply, and overhaul capabilities.