Cooling, conveying and metal detecting

Conveyor belts are a vital part of manufacturing and today, offer varied roles in food production. International Confectionery explores them….

Share this article:

Conveyor belts are a vital part of manufacturing and today, offer varied roles in food production. International Confectionery explores their varying uses and important considerations.

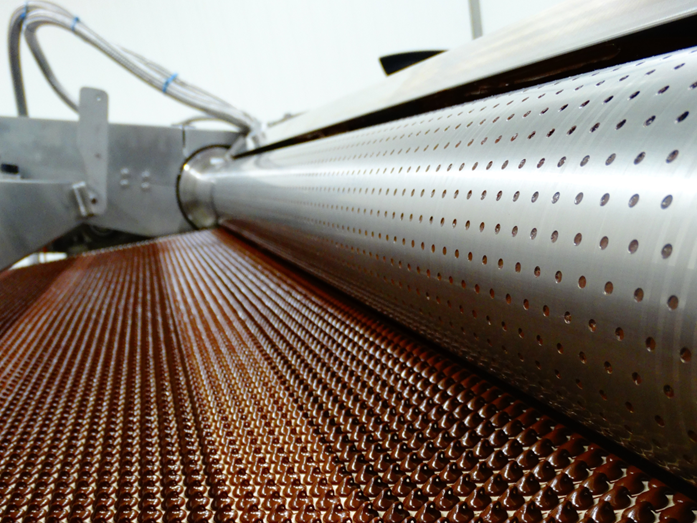
Conveyors are vital for conveying raw materials and end products for confectionery during the production process, but there are a number of factors which need to be considered when picking what conveyor belts to implement. During the production process confectionery products like toffee or chocolate often have sticky textures, so the conveyor needs to be made from a material which is capable of handling sticky textures with easy release, to reduce the likelihood of the product sticking to the belt. Whether this is an end product or bulk raw materials that are being conveyed, the wide range of conveyor belts are able to handle this, as well as cooling conveyors and conveyors capable of metal detection which reflect the variety of roles they can provide in manufacturing.  

Conveying systems don’t take just one shape in the food and beverage industry, as the processes themselves are varied. Common types used today include belt conveyors, vibratory conveyors and tubular cable drag conveyors. Basic conveyor belts work to transport confectionery products throughout the production process. Processes such as enrobing, cooling, packaging, coating, metal detection and check weighing can all be achieved thanks to the implementation of conveying systems.

Vibratory conveyors work well for transferring sticky confectionery products and any other difficult bulky products by using vertical motion. The conveyor moves upward at a particular angle and in doing so, lifts the product which is then moved forwards through each vibration. When determining which vibratory conveyor to use, this will depend on the kind of product being conveyed, how much of it will be conveyed, and at what speed it needs to be conveyed: all of this information will provide a better picture of the conveyor required. Tubular drag conveyors are commonly used in transporting bulk materials, as they use a chain and disc assembly to pull or drag material along in a sealed tube. 

It goes without saying that the hygiene of conveying systems is imperative as they come into contact with food. Conveyors are designed based on criteria related to the overall hygiene required for the production facility, the products that will be processed, as well as a HACCP plan and hazard analysis. Considerations for the manufacturing of conveying systems need to focus on making the system easily accessible for inspection and maintenance, the materials need to be made with tension resistant, water-tight and non-absorbent materials to reduce the risk of contamination, and need to be smooth and resistant of any cracks and crevices to prevent microorganisms from growing in the cracks...

To read more see our latest issue here.

Media contact

Caitlin Gittins
Editor, International Confectionery
Tel: +44 (0) 1622 823 920
Email: [email protected]
About International Confectionery

International Confectionery is the leading authority in global confectionery content, delivering expert news, in-depth articles, exclusive interviews, and industry insights across print, digital, and event platforms. Published 10 times a year, the magazine is a trusted resource for professionals seeking updates and analysis on the latest developments in the confectionery sector.

To submit an article, or for sponsorship opportunities, please contact our team below.

Joseph Clarke Picture

Joseph Clarke

Senior Editor

Steve Blakebrough Picture

Steve Blakebrough

Sales Manager

Afua Akoto Picture

Afua Akoto

Marketing Manager

Related News

Nexture Sustainability

Nexture Publishes First Sustainability Report

Nexture has published its first Group Sustainability Report, establishing a shared framework for reducing environmental impacts, improving responsible sourcing and developing more sustainable ingredient solutions.
ipco pack expo

IPCO Unveils Chocolate Forming Solutions

IPCO, a supplier of chocolate forming and moulding equipment, showcased its latest innovations at PACK EXPO 2026, emphasizing advancements in chocolate chip production and cooling systems.
Domori

Domori Launches in the UK

Italian chocolate producer Domori has introduced its professional couverture chocolate range to the UK, targeting chocolatiers, pastry chefs, gelato makers and other specialist dessert producers.
KitKat Nestle

KitKat Drives Formula 1 Excitement

Nestlé International Travel Retail (NITR) has brought the excitement of the KitKat and Formula 1® partnership to travellers at Singapore Changi Airport through a high-impact activation combining immersive brand experiences, personalisation and travel retail-exclusive products.
EXBERRY colour selection

GNT Secures ISO Carbon Verification

GNT has become one of the first food colour manufacturers worldwide to have its Product Carbon Footprint (PCF) methodology independently verified in line with the ISO standard.
NSD

Celebrating US National Real Sugar Day

The Sugar Association will celebrate National Real Sugar Day on October 15 by recognising real sugar’s role as a real, recognisable ingredient in real food. This year’s celebration also highlights that real sugar is rooted in nature and is at the heart of real recipes and scratch cooking.
Anuga India

SACMI highlights integrated chocolate processing

SACMI Packaging & Chocolate is showcasing its latest chocolate processing and packaging technologies at Anuga FoodTec India 2026, highlighting an integrated portfolio spanning production, wrapping, handling and secondary packaging.
Anuga India

Anuga FoodTec India is Open

Anuga FoodTec India 2026 has opened its doors in Mumbai, bringing together food and beverage technology suppliers from around the world for three days of processing, packaging and manufacturing innovation.
Scroll to Top