
International Confectionery Technical Editor, Clay Gordon, explores the world of biscuit production and the enrobing process involved in this.
Over the course of the past decade, I have advised many small businesses on the purchase of enrobing lines, or more commonly, enrobing belts as an accessory to a continuous tempering machine.
By far the most common misconceptions I must address are ones related to size – and this is a case where bigger is not necessarily better. Most first-time buyers don’t have a good grasp of the relationships between belt width and speed, desired production throughput, the capacity of the tempering machine required to meet the desired throughput, capital equipment costs, labour costs and finally, how much cooling capacity is required.
These factors are interdependent; changing one assumption usually requires revisiting several other assumptions. Increasing capacity is not just a matter of increasing belt width or speed. These two factors need to be weighed against the amount of chocolate required, how much labour is required (how many people are needed), and how cooling is going to be achieved. Sometimes it’s more cost efficient to spend money on equipment in order to save money on other operational costs such as ground rent and energy.
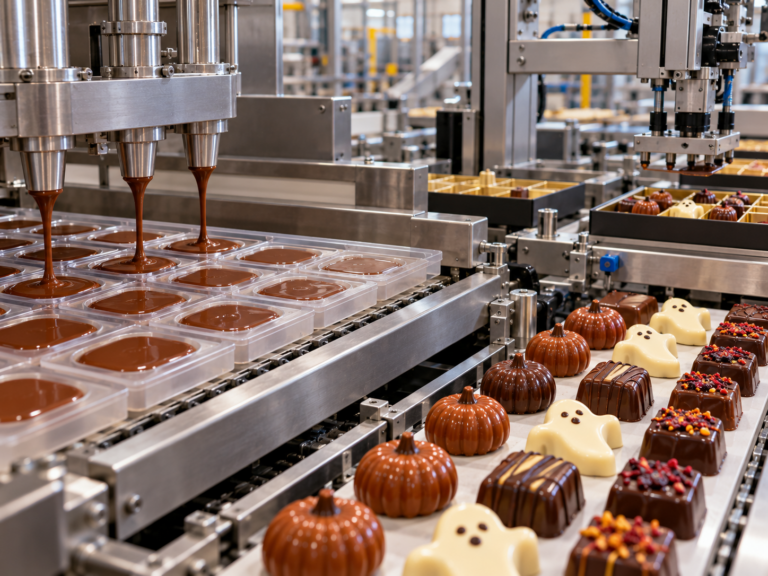
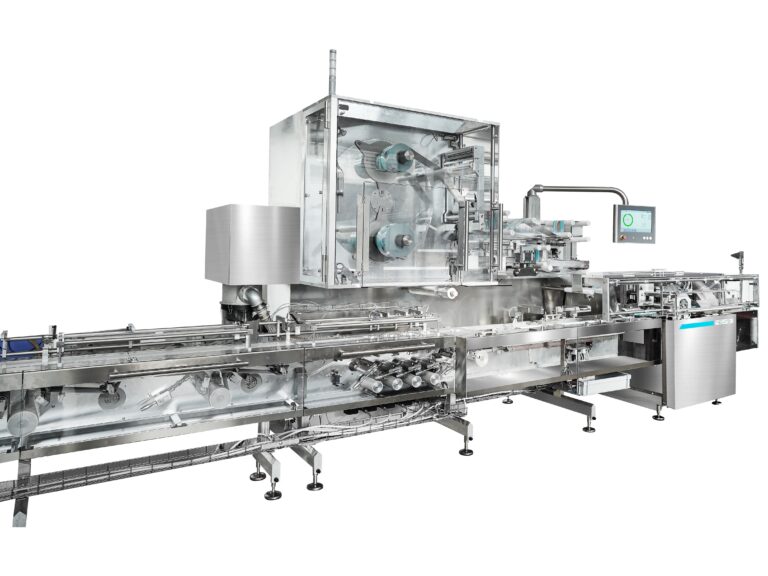
It’s helpful at this point to step back and consider the different elements of any enrobing line, no matter how big.
The entrance section is where the pieces to be enrobed are placed. It is usually made of metal wire.
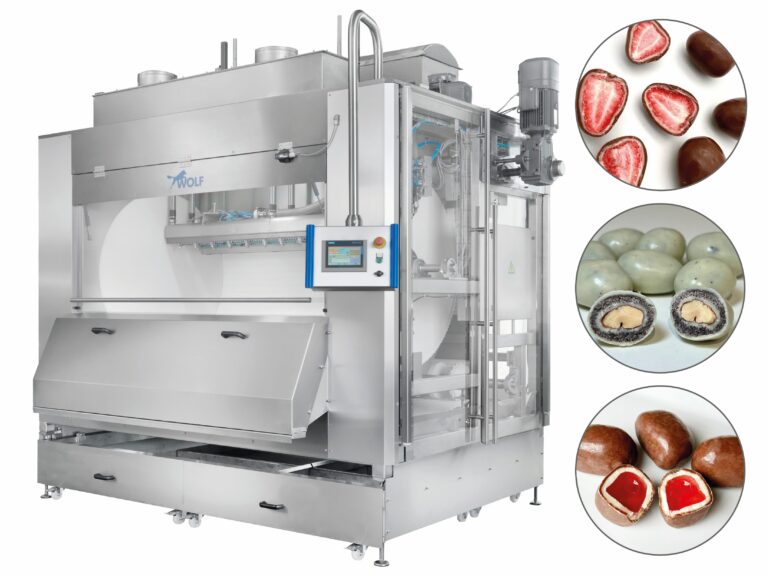
The working section is where the pieces are bottomed (if needed) and covered with chocolate. After the bottoming and covering steps, it is usual for there to be a net beater and a blower to remove excess chocolate. Because the chocolate needs access to all sides of the piece and excess chocolate needs a place to go, the working section of the belt is also made of metal wire. Finally, at the end of the working section is the detailer, a spinning rod that removes excess chocolate from around the bottom edges of the chocolate, reducing the size of feet that might form.
The exit, or take-off section, follows. On small enrobing lines, this is a plastic belt with a support for a roll of coated take-off paper that facilitates the removal of pieces before the chocolate is set. On a larger line there may be no separate take-off section. Instead, the enrobed pieces go straight on to a food-grade plastic belt that forms the entrance section of a cooling tunnel.
There are many variations in this basic design. One question to be addressed is how (or if) the pieces will be decorated, the answer(s) to which will determine what kinds of other equipment and sections, if any, need to be added to the line. Other accessories that are common on enrobing lines are copes (enclosures) around the main working section, often with heat sources that help regulate and maintain a constant temperature; partial enrobing plates, the ability to bottom only, mechanisms to flip pieces upside down (common when bottoming baked goods), mechanisms to sprinkle toppings such as flaked coconut and more.
Read more of our latest edition here: March 2022 Single Issue form – International Confectionery Magazine (in-confectionery.com)
Media contact
Roshini Bains,
Editor, International Confectionery
Tel: +44 (0) 1622 823 922
Email: [email protected]